


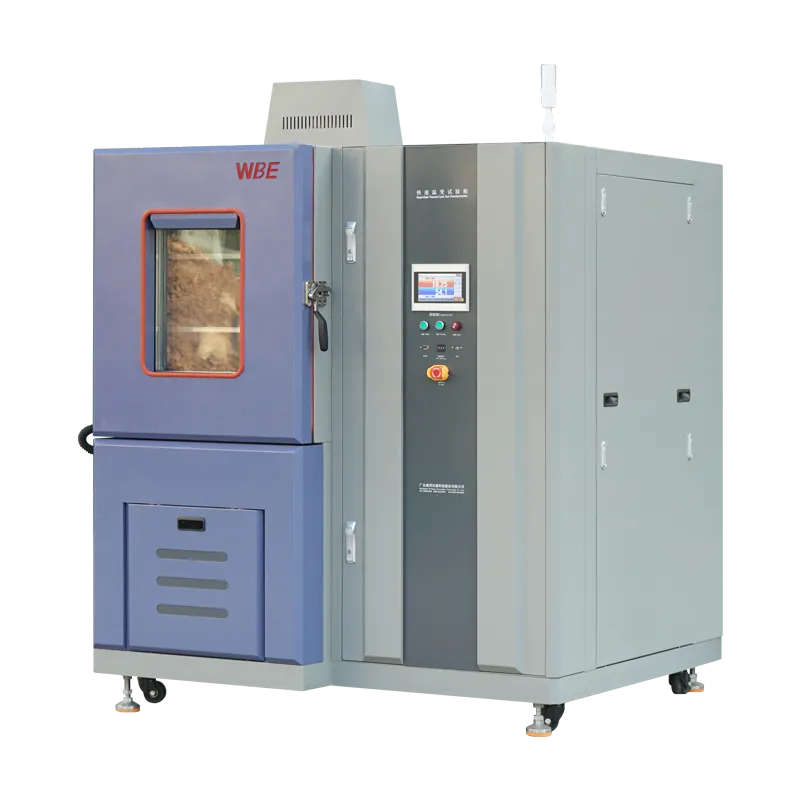
A rapid rate temperature exchange chamber is a production instrument, not a development instrument, and confusing those two roles is the most expensive mistake we see in environmental stress screening. ESS exists to catch manufacturing defects on a design you have already validated, using a profile you have already proved. HALT exists to break a design on purpose so you can find its weak points before you commit to volume. The hardware can look almost identical on the shop floor. The purpose, the profile, the sample size and the treatment of a failure are all different.
This guide follows the order a screening programme is actually built, and it answers the question almost every customer asks us: is a faster chamber the fix, or is the workflow around it the real constraint? We will cover five things in sequence: separating the two purposes, designing the screen profile, choosing the sample size and the accept rule, fitting the screen to the line rhythm, and deciding when HALT is the right tool and when it is not.
The short version, if you only read this far
- ESS screens assembled units against a fixed profile; HALT searches for a design limit with an increasing one.
- In ESS a failure is a defect signal about the process; in HALT a failure is the deliverable.
- A screen is a budget of fatigue life, so it must be validated on known good and known bad samples.
- Chamber cycle time is rarely the real bottleneck; loading and fixture cooling usually are.
Step 1: Separate the Two Purposes Before You Compare Hardware
ESS and HALT use similar stress types but point in opposite directions, so the first decision is not which chamber to buy but which question you are answering. Environmental stress screening asks whether this particular unit was assembled correctly. HALT asks what the design can survive. One is a control on production, the other is an experiment on engineering, and every downstream choice follows from that split.
| Dimension | Environmental stress screening | Highly accelerated life testing |
|---|---|---|
| Purpose | Detect manufacturing defects in units already designed | Expose design weaknesses and find operating limits |
| When it runs | In production, on an established profile | During development, before the design is frozen |
| Profile | Fixed and validated, chosen to avoid damaging good product | Stepped and increasing, deliberately pushed until failure |
| Failure handling | The unit is rejected and the process is investigated | The failure is the result, and the design is improved |
| Success looks like | High yield through the screen, no escapes to the field | A clearly identified limit and a corrected design |
Read the failure row twice. A team that treats an ESS failure as a design finding will spend weeks chasing a root cause that lives in a soldering oven. A team that treats a HALT failure as a process problem will quietly ship the same design weakness into production, one that no screen was ever going to catch. Once the purpose is written down, the next job is to build the profile that serves it.
Step 2: Design the ESS Profile Inside a Rapid Rate Temperature Exchange Chamber
A screening profile is a budget of fatigue life, so the job is to spend the smallest amount that still catches the defect you care about. Four settings define that budget, and they should be chosen from the defect rather than from whatever the previous product used. Get them right and marginal units fail while good units keep margin; get them wrong and you either pass bad product or create failures in product that was never the problem.
- Temperature extremes. Wide enough to load the defect, narrow enough that a healthy unit is not pushed toward its own limit.
- Dwell time. Long enough for the slowest part of the assembly to actually reach temperature. A dense power module with a heavy heat sink can still be climbing internally while the chamber air has already settled.
- Cycle count. Enough repetitions to accumulate strain at the target defect, and no more than the good unit can absorb with margin.
- Transfer rate. Driven by the mechanism you are chasing, and expressed honestly in the mode the machine will actually run.
That fourth item deserves its own paragraph, because it is where specifications mislead. Our rapid change platforms support two modes, and they are not the same promise. Linear means the rate is held through the whole transition. Average non-linear means the quoted figure is an average across the move, with faster and slower portions inside it. If your defect responds to the peak rate rather than the average, a profile written as linear and a profile written as average can behave quite differently on the same machine, so the mode belongs in the test plan, not only in the purchase order.
The test we apply to any proposed screen: name the defect it should catch, then show us a unit that contains it and a unit that does not. If the screen cannot tell those two apart, no amount of chamber capability will make it useful, and it is cheaper to discover that on twenty samples than on twenty thousand.
Before a screen goes live, prove it against known bad and known good samples, then confirm that good units survive with room to spare. Only once the profile separates those groups is it worth asking how many units to run through it, which is the next decision.
Step 3: Set the Sample Size and the Accept Rule
Screening every unit and sampling a lot protect against genuinely different risks, so the choice should follow the cost of a field failure rather than the capacity of the line. Full screening catches unit level escapes, including the single badly assembled part inside an otherwise healthy batch. Sampling catches process drift, but it will never see that one bad unit.
| Approach | What it protects against | Where it breaks down |
|---|---|---|
| Full screen, every unit | Unit level escapes, including one off defects | Costs line time on every unit and needs capacity to absorb it |
| Lot sampling | Process drift and batch level problems | Misses the single badly assembled unit inside a good lot |
| Sampling plus process monitoring | Drift, plus a defined trigger to escalate to full screening | Requires the discipline to escalate when the data says so |
Most unhappy programmes we are asked to review live in the middle row. Sampling looks like a sensible compromise until a field return traces back to a unit that was never screened, and then the whole approach is re-examined under pressure. The accept rule matters just as much as the sample size. Decide in advance what a failure means, who investigates it, and what evidence upgrades a run from sampled to full, because a rule invented after the first failure is a rule written by whoever is most worried that day.
With the profile validated and the accept rule fixed, the remaining question is whether the line can actually feed the screen at the rate you need, which is where most throughput complaints really begin.
Step 4: Fit the Screen to the Line Rhythm
Chamber cycle time is rarely the real bottleneck, and choosing an equipment rate before modelling the workflow is how money gets spent twice. A rapid rate temperature exchange chamber that spends a third of every cycle waiting for a fixture to cool, or for the next batch to be staged, is being paid for and then idled. The rate only helps once the machine is genuinely the limiting station.
That is where the available rate steps do real work. Our platforms offer 5, 10, 15, 20 and 25 °C/min, and each step buys a different station time for the same temperature swing. Running at a higher step shortens the transition, which shortens the cycle and raises the number of cycles per shift, but it only converts into throughput if the loading, the electrical test and the fixture cooling can keep pace. The honest way to choose is to time a full cycle on the line, from unload to next load, and then see how much of it is chamber and how much is everything else.
One supplier we worked with on an automotive programme had exactly this problem. Their throughput complaint was blamed on the chamber, but their fixture needed a full cool down before the next batch could be secured, and the chamber sat idle for a large part of every cycle. Redesigning the fixture so the next batch could be pre-staged mattered far more than any change to the ramp rate, and it was a fraction of the cost of new equipment. Only after that did a rapid temperature change chamber make sense, because by then the chamber really was the constraint.
The same logic applies when two stress types are needed. If the defect is driven by a combination of thermal and mechanical load, splitting them across two stations adds handling time and adds a chance of damaging the unit between steps. That is why combined platforms such as a rapid temperature and vibration test system exist: they remove a station instead of adding one. Automotive electronics supply chains tend to reach that point earlier than others, and our automotive application page describes how those programmes are usually arranged.
Two more habits are worth writing into the plan. Add humidity only when moisture or corrosion is the target defect, because a rapid change wet heat test chamber earns its place when that is the case and adds cost and cycle time when it is not. And keep pass rate by lot, because without that record a rising escape rate looks like noise until it becomes a recall. Once the screen is stable and understood, the last question is when to reach for a different tool entirely.
Step 5: Know When to Go to HALT, and When Not To
HALT is the right tool when the design is still moving and you need to know where it breaks; it is the wrong tool when the design is frozen and the question is whether this unit was built correctly. Reaching for HALT on a production line ramps stress up until units fail, which destroys good product and teaches you almost nothing about the design, because the sample is not representative and the failures are not controlled.
- Use HALT before the design freezes, on a small number of units, when you want to expose a limit and improve the product.
- Use screening after the design freezes, on a validated profile, when the question is process quality rather than design quality.
- Refuse HALT as a production gate, because an increasing stress ramp applied to every unit is a plan to destroy good product and call it data.
- Refuse screening as a design investigation, because a fixed profile cannot tell you the limit of a design, only whether a unit behaved like its siblings.
One machine can often do both jobs, and many development labs run exactly that way. The caution is procedural rather than mechanical: the profile, the sample selection and the reaction to a failure must all change between the two activities, and that has to be written down. Otherwise the production team inherits a development habit, and the line quietly starts turning good units into scrap. If you would like a second opinion on which of the two you are actually running, our solutions team works through that question with customers before any equipment is specified.
Frequently Asked Questions
Can one rapid rate temperature exchange chamber serve both ESS and HALT?
Often yes, and many development labs do exactly that. The caution is procedural rather than mechanical. The profile, the sample selection and the way you react to a failure must all change between the two activities, and that must be written down, because otherwise the production team inherits a development habit and the line starts rejecting good units.
How much of the product life does a screen consume?
It depends entirely on the profile and the assembly, and any figure quoted without both of those details should be treated with suspicion. The principle is straightforward: the screen should consume a small fraction of expected life so good units pass with margin, while still being aggressive enough to expose a clearly defective one. That balance is found by testing known good and known bad samples, not by calculation alone.
Should every unit be screened?
If a unit level defect can reach the customer and the consequence is serious, yes. Sampling protects you against a drifting process, not against one badly assembled unit inside an otherwise healthy lot. Where the failure consequence is high, full screening with a validated profile is usually the more rational choice once the cost of a field return is counted honestly.
What is the most common mistake on a screening line?
Buying a faster chamber before fixing the handling. In most lines we have reviewed, the stress step was idle for a significant part of every cycle while fixtures were swapped and batches were staged. A chamber upgrade applied to a workflow problem does not add capacity, it just moves the queue to a different place.
A rapid rate temperature exchange chamber earns its place on a production line only when the programme around it is clear about what it is doing. If the goal is to catch assembly defects on a validated design, it is a screening tool and the profile must be fixed, validated and repeatable. If the goal is to find the limits of a design that is still moving, it is a development tool and the failures are the deliverable. Decide which one you are running before you specify the equipment, and the machine will do exactly what you need it to do.
Build the screen before the product reaches the line
Browse rapid change and combined stress platforms used in production screening, listed by chamber construction and controller options so you can compare them against your real line rhythm.
Browse screening chamber models Talk through your ESS plan